Medical Equipment Wire Harness Introduction
As a professional medical equipment wiring harness manufacturer, Nanguandi Electronics Co., Ltd. focuses on providing high-quality, high-reliability and customized medical wiring harness solutions for global medical device manufacturers.
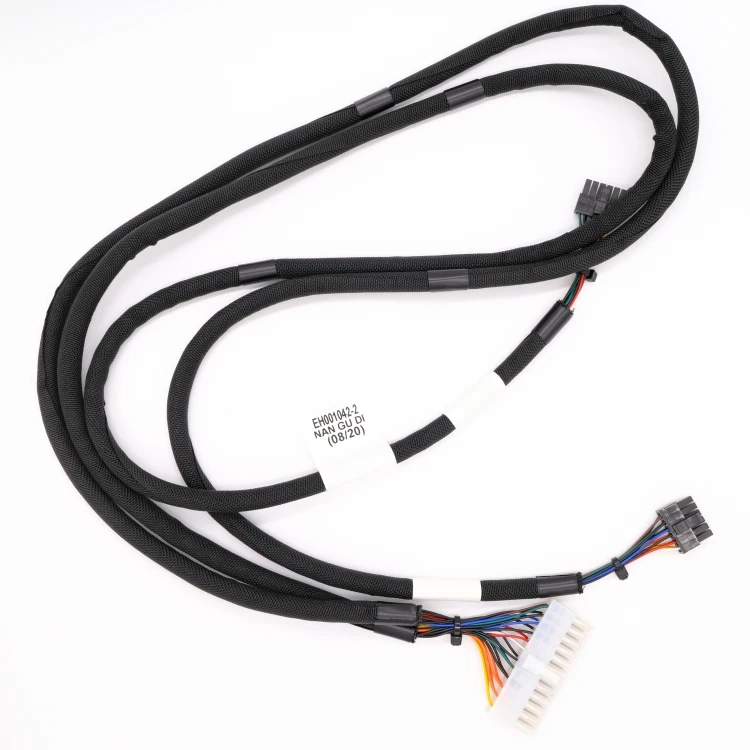
Medical wiring harnesses serve as core carriers for power transmission, signal delivery and data interaction inside medical devices. Being an indispensable key component of modern medical equipment, they directly determine the operational stability, accuracy and safety of medical devices. They are widely applied in diagnostic equipment including CT scanners, MRI systems and ultrasonic diagnostic instruments, therapeutic equipment such as laser therapy devices, hemodialysis machines and electrosurgical instruments, monitoring devices like ECG monitors, blood pressure monitors and multi-parameter monitors, as well as auxiliary medical devices covering medical infusion pumps, medical ventilators and sterile supply equipment.
Different from ordinary industrial wiring harnesses, our medical-grade wiring harnesses fully comply with international medical standards and meet special requirements of medical environments, featuring excellent biocompatibility, chemical corrosion resistance, dustproof, moistureproof and strong anti-electromagnetic interference performance.
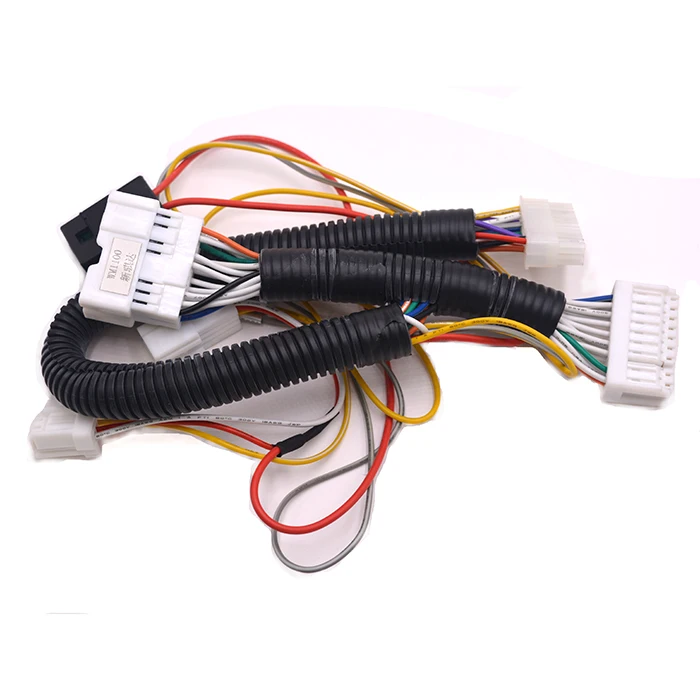
Integrating power wires, signal wires, control wires and sensor cables, our products can accurately connect core components such as mainboards, sensors, actuators and display modules of medical equipment, realizing stable power supply, real-time signal transmission and precise data interaction.
Against the backdrop of advancing medical technology, growing aging population and rising demands for medical services, Nanguandi Electronics continuously upgrades technologies and optimizes production processes to meet the booming market demand for high-standard and high-reliability medical wiring harnesses.
We customize wiring harnesses according to the internal structure, installation space, service environment and interface specifications of different medical devices. In strict accordance with GMP good manufacturing practices and QMS quality management system, our products deliver stable and reliable performance, effectively solving common problems such as wire fracture, signal distortion, insulation failure and poor corrosion resistance. We provide solid and safe circuit support for stable operation of medical equipment, and fully safeguard patients’ health and safety.
Adhering to the principle of Safety First, we adopt medical-grade eco-friendly materials for all medical wiring harnesses. Parts in contact with human bodies or medical liquids contain no toxic and harmful substances, causing no irritation or allergic reactions to avoid potential risks to patients. All raw materials pass strict safety tests including flame retardancy, non-toxicity and environmental protection, fully conforming to international medical industry standards and satisfying double protection requirements for both patients and operators. The insulating layer is made of high-performance flame-retardant materials with outstanding self-extinguishing capability, effectively eliminating safety hazards such as short circuits and electric leakage, which is our core commitment to medical equipment operation and patient safety.
Medical devices like CT scanners and MRI equipment impose extremely high requirements on signal transmission accuracy. Our medical wiring harnesses can effectively isolate external electromagnetic interference and internal electromagnetic clutter, preventing signal crosstalk, data deviation and signal delay to ensure lossless transmission of sensor signals, control signals and high-speed data signals. Adopting high-purity oxygen-free copper conductors, our products feature low conductive loss and stable signal transmission, enabling medical equipment to accurately collect patient data, send control instructions and display diagnostic results.
The outer protective sheath is made of self-selected high-performance materials with superior corrosion resistance, moisture resistance and high temperature resistance. It can resist erosion by common medical disinfectants such as alcohol and antiseptic solution, and stably work within the temperature range of -40℃ to 125℃ without hardening, embrittlement or insulation failure during long-term service. Meanwhile, the excellent dustproof property prevents dust and sundries from entering wire cores to avoid circuit blockage and signal faults. This is the practical solution we developed after in-depth research on medical application scenarios.
For frequently movable and angle-adjustable medical equipment, our wiring harnesses are manufactured with high-flexibility conductors and elastic insulating materials. They can withstand millions of repeated bends and multi-angle torsion, free from wire breakage, sheath damage and structural failure in long-term use.
Fully aware of diversified medical device models and differentiated harness requirements from different manufacturers, we provide comprehensive customized services for medical wiring harnesses, covering wire length, core specification, branch layout, terminal models, connector types and wiring definitions. We can produce integrated, split-branched and hidden thin wiring harnesses of various styles. Our customized harnesses fit perfectly with the internal wiring layout of medical devices, featuring neat and orderly arrangement to facilitate equipment assembly, daily maintenance and later upgrading.
Medical equipment usually needs long-term continuous operation, which sets extremely strict standards for harness stability and precision. Our medical wiring harnesses are manufactured via sophisticated production techniques and rigorous quality control with precise dimensional tolerance and stable overall performance. Every finished product undergoes complete electrical performance tests including voltage resistance, continuity and insulation tests before delivery, ensuring long-term stable operation during continuous service and guaranteeing smooth medical work.
Production Strength & Quality Control
We have a professional raw material procurement and testing team, strictly selecting medical-grade raw materials in line with international medical standards, including high-purity oxygen-free copper conductors, medical flame-retardant insulating materials and biocompatible protective sheaths. Every batch of raw materials is thoroughly inspected to meet strict quality standards for medical wiring harnesses. Equipped with advanced fully automatic numerical control wire cutting and stripping equipment, we control cutting length and stripping depth accurately within a tolerance of ±0.1mm, avoiding core damage and uneven stripping to lay a solid foundation for product precision and quality.
We adopt internationally advanced constant-pressure integrated crimping technology for wire core and terminal connection, ensuring tight, firm and gapless connection without virtual welding or loose contact to stabilize power and signal transmission. High-precision welding technology is applied to key component connections, featuring firm welding and low contact resistance to prevent signal loss and power supply failure. All finished products are subject to strict tension tests and continuity inspections after crimping and welding, guaranteeing stable connection performance under equipment movement and vibration conditions.
Based on the service characteristics of various medical devices, our technical team adopts differentiated binding treatments for movable and fixed areas of wiring harnesses. Flexible medical-grade wrapping tapes are used for movable parts to retain bending flexibility and avoid damage caused by repeated movement; standardized wiring shaping is applied to fixed parts to prevent wire winding and friction during equipment operation, improving overall protection and tidiness while lowering circuit failure risks.
We attach great importance to finished product inspection. All medical wiring harnesses must pass a full range of strict simulation tests before delivery, including bending fatigue test, high and low temperature cycle test, chemical corrosion test, signal stability test, insulation test and voltage resistance test. Defective products are strictly eliminated to ensure all delivered products meet high-standard application requirements of medical equipment.
Our medical wiring harnesses are packed independently in sterile, moisture-proof, dustproof and shockproof packages to avoid contamination during production and packaging. Exclusive customized protective packages are adopted for tailor-made products to prevent extrusion deformation, interface damage and pollution in transit. We also provide matched wiring accessories and installation auxiliary materials for one-stop delivery, enabling convenient direct installation and ensuring sterility and intactness during transportation and installation.
We have established a complete full-process quality management system covering the whole production chain of medical wiring harnesses. Professional quality inspectors conduct strict inspections in every link from raw material selection, production processing to finished product delivery. We strictly implement GMP good manufacturing practices and QMS quality management system with detailed production records to realize full product traceability, ensuring all medical wiring harnesses feature stable performance and reliable quality to fully satisfy high-standard demands of medical equipment.
 ×

 EN