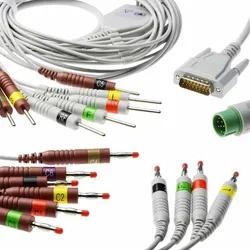
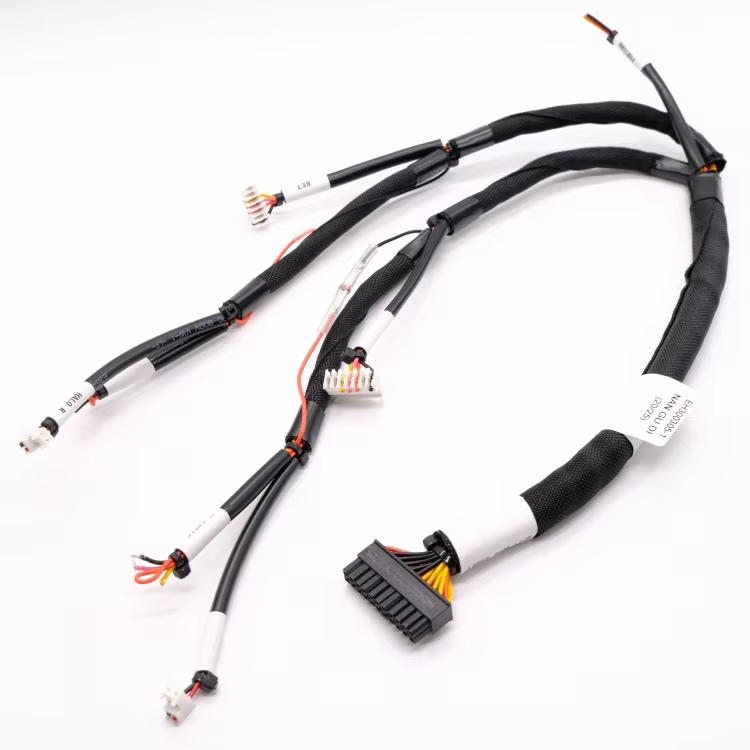
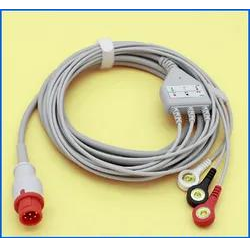
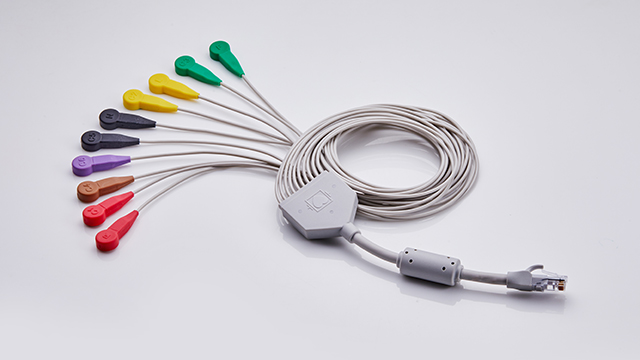
Medical signal wiring harnesses are the backbone of modern healthcare technology, ensuring that critical data from sensors, electrodes, and imaging equipment is transmitted accurately and without interference. At WEITAI, we have dedicated over two decades to perfecting the art of custom wire harness manufacturing. Founded in 2006, our company has grown into a national high-tech enterprise and a "Little Giant" in Guangdong Province, a status reserved for specialized and innovative firms. With two production bases in Humen, Dongguan, spanning 12,000 square meters, and a subsidiary in Hong Kong, we are strategically positioned to serve the global medical device industry.
Our manufacturing capabilities are backed by certifications including ISO9001, ISO13485 (medical devices), IATF16949 (automotive), and UL. This ensures our medical signal wiring harnesses meet the highest regulatory standards, essential for medical devices that require reliability and safety. We employ 316 professionals, including 35 R&D engineers, who work in tandem with our clients to design solutions that address specific application challenges. Our R&D team has over 40 patents, giving us a competitive edge in innovative harness designs.
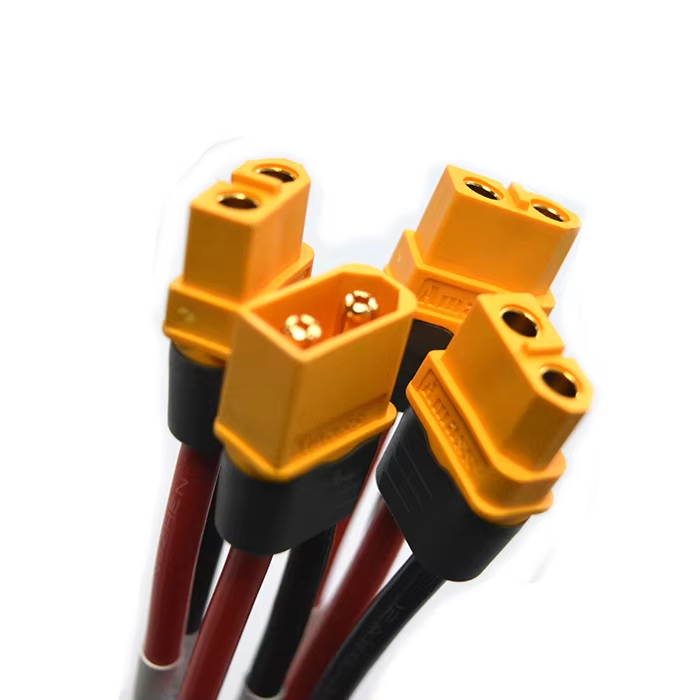
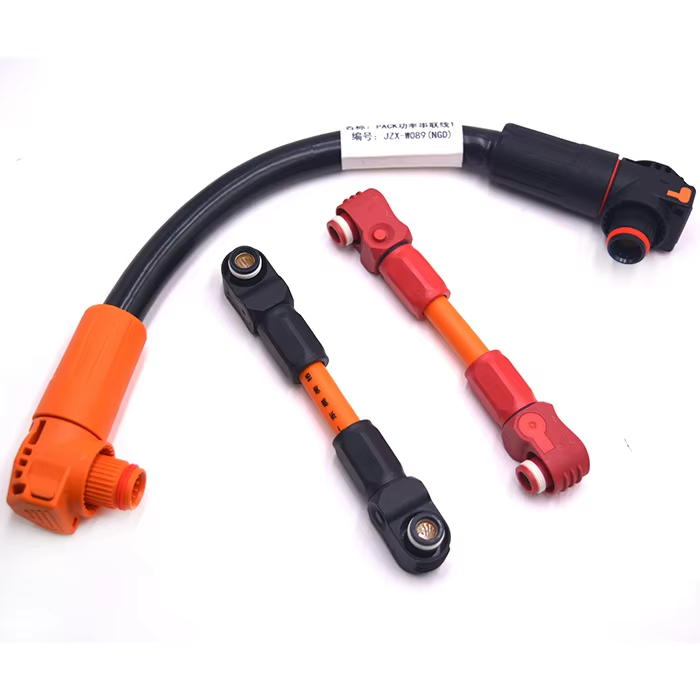
In the medical field, signal harnesses must handle low-level voltages, microvolt signals, and high-frequency data while resisting electromagnetic interference (EMI) and radio-frequency interference (RFI). Our harnesses are constructed with premium materials such as PTFE, PVC, and cross-linked polyethylene, selected for their insulating properties and biocompatibility. We offer a range of connector options, from 24-pin high-density connectors to custom terminal configurations, ensuring compatibility with your device architecture.
One key differentiator is our commitment to quality control. Every batch undergoes 100% electrical testing, including continuity, insulation resistance, and hi-pot testing. Our quality rate consistently exceeds 98%, as evidenced by our annual defect rate of 0.1%. For instance, in a recent order of 10,000 harnesses for a ventilator manufacturer, we achieved a 99.5% first-pass yield, significantly exceeding industry norms.
Moreover, we understand the importance of data security and supply chain resilience. Our dual production bases and robust supply chain management ensure that we can accommodate sudden demand spikes, as witnessed during the COVID-19 pandemic when we rapidly scaled up production of medical harnesses for respirators and monitoring devices. We delivered 200,000 units in three months, with a 100% on-time delivery record.
Our global reach includes partnerships with medical device OEMs in Europe, North America, and Asia. For example, we supply a leading ICU monitor manufacturer with over 50,000 harnesses annually, helping them maintain a 99.9% uptime for their devices. Our engineers are experts in navigating international regulations, including IEC 60601-1, and we provide comprehensive documentation to facilitate your certification process.
When you choose our medical signal wiring harnesses, you benefit from:
Custom design & development with rapid prototyping (lead times as short as 3 days).
Full backward and forward traceability of materials and processes.
Competitive pricing without compromising quality—typically 10-15% lower than equivalent Western manufacturers.
Logistics support with Incoterms flexibility, ensuring smooth delivery to your facility.
We are not just a supplier; we are your strategic partner in medical innovation. Our team is ready to support you from concept to production, ensuring that your medical devices perform optimally and, most importantly, positively impact patient lives.

 EN