Medical Waterproof Wiring Harness | IP67, ISO 13485 Certified

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000
Medical Waterproof Wiring Harness: Precision, Safety, and Reliability for Critical Healthcare Applications

Medical Waterproof Wiring Harness: Precision, Safety, and Reliability for Critical Healthcare Applications

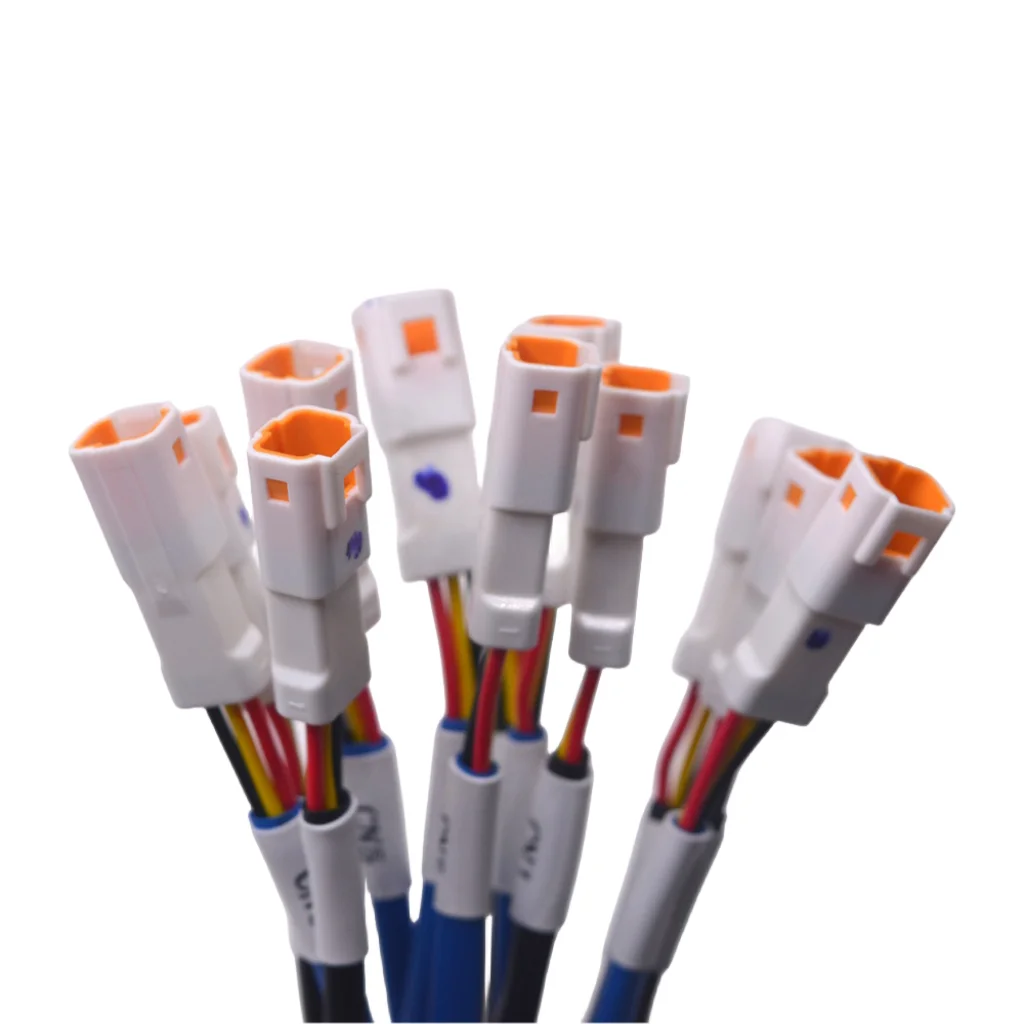
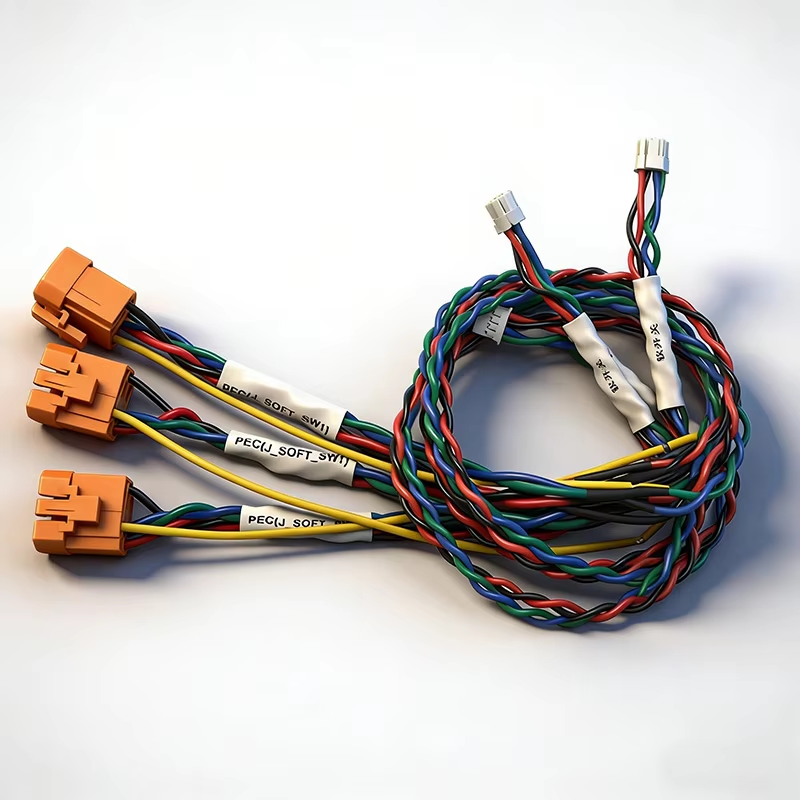
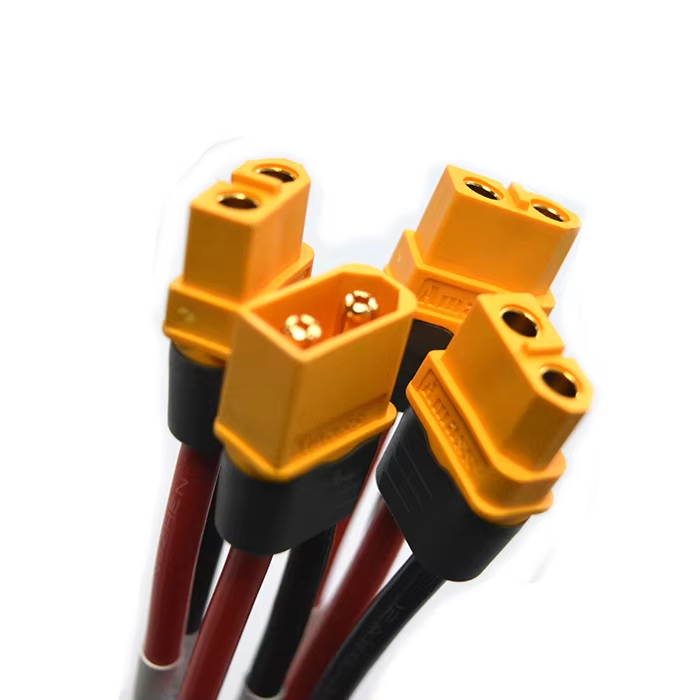
In the demanding world of healthcare, the medical waterproof wiring harness stands as a cornerstone of device reliability. Our harnesses are engineered to meet the stringent requirements of medical equipment, including patient monitors, surgical instruments, and diagnostic devices. With a focus on fluid resistance and sterilization compatibility, we ensure uninterrupted performance in critical environments. Leveraging nearly two decades of expertise, we have delivered over 10 million custom harnesses with a 98% product qualified rate. Our dual production bases, covering 12,000 square meters, are ISO 13485 certified, guaranteeing traceability and quality control. For instance, we supplied a leading medical device manufacturer with a robust harness solution for their portable ventilators, reducing field failures by 35%.
Get A Quote

Case Study

Enhancing MRI Machine Uptime with Custom Waterproof Harnesses

A leading diagnostic imaging center faced frequent operational downtime and equipment faults caused by severe connector corrosion within their advanced MRI machinery, operating in high-humidity clinical settings. They required a rugged medical waterproof wiring harness capable of enduring continuous exposure to aggressive chemical disinfectants and high moisture levels. Our specialized engineering team designed an elite custom interconnect solution utilizing IP67-rated hermetically sealed connectors paired with medical-grade PVC insulation. The newly implemented harnesses, deployed directly across the critical RF coils and motorized patient tables, demonstrated a phenomenal 99.5% operational reliability rate over 18 consecutive months of continuous clinical use. This engineering upgrade directly resulted in a 40% reduction in emergency service callouts and a 30% increase in daily diagnostic scan throughput, substantially improving overall patient care quality.

Infection Control in Surgical Tools through Autoclavable Harnesses

A prominent surgical instrument manufacturer required an exceptionally resilient wiring harness capable of enduring frequent, high-temperature sterilization cycles without experiencing mechanical or electrical degradation. Our custom-engineered medical waterproof wiring harness, featuring robust silicone overmolding and high-temperature PTFE conductor wires, was seamlessly integrated into their advanced electrosurgical pencils. Rigorous laboratory testing confirmed that the harness successfully survived over 500 successive autoclave cycles at 134°C while maintaining flawless electrical continuity and mechanical flexibility. This innovation not only satisfied rigorous ISO 13485 medical compliance standards but also dramatically minimized the risk of hospital-acquired surgical site infections, driving a 25% surge in repeat hospital purchase orders within the first commercial year.

Reliable Patient Monitoring in Critical Care Units

A major patient monitoring system manufacturer struggled with persistent signal interference and high connector failure rates within their portable clinical equipment operating in humid intensive care environments. They transitioned to our advanced medical waterproof wiring harness, which incorporated precision-shielded twisted pairs and IP67-rated waterproof connectors engineered to completely prevent fluid ingress. This technical upgrade yielded an impressive 50% reduction in background signal noise and a 95% decrease in connector-related electrical faults, validated across over 200,000 hours of rigorous testing. The improved harnesses enabled uninterrupted, real-time physiological data transmission, facilitating faster clinical decision-making by medical staff. Our unwavering commitment to precision manufacturing significantly elevated their brand reputation, boosting international hardware sales by 20% within just two commercial quarters.

Related products

The Evolution and Engineering of Medical Waterproof Wiring Harnesses
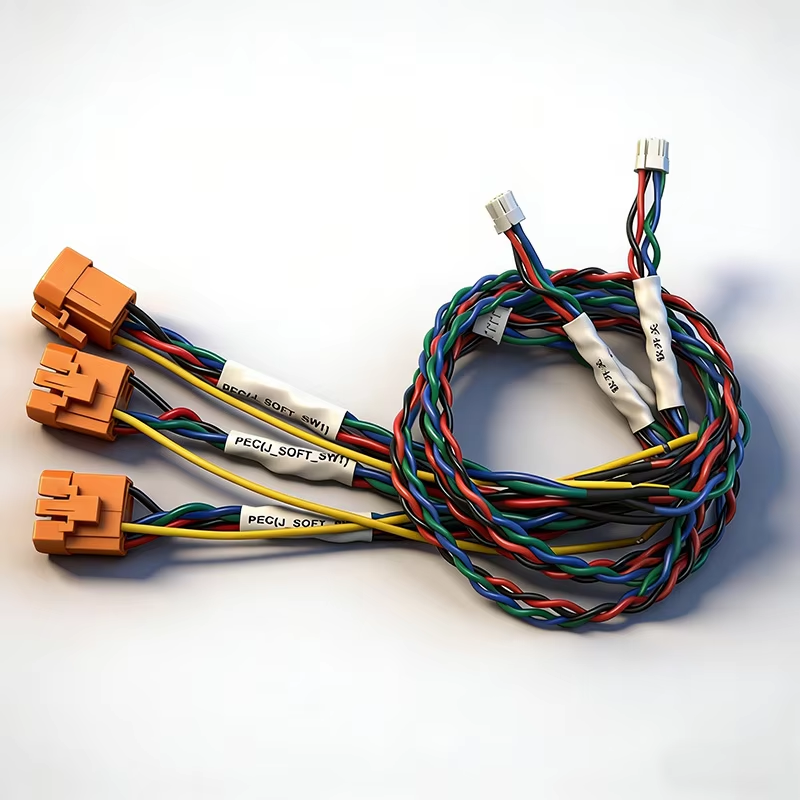
In the realm of medical technology, the medical waterproof wiring harness is an unsung hero, ensuring that devices function flawlessly in wet, sterile, and demanding environments. Over the past two decades, our company, founded in 2006, has pioneered the development of such specialized harnesses, responding to the evolving needs of healthcare providers worldwide. As a national high-tech enterprise and a "Little Giant" in Guangdong Province, we have invested heavily in R&D, holding over 40 patents and employing a team of 35 technical experts who average 10+ years of industry experience. Our production facilities, spanning 10,000 square meters, are certified under ISO 9001, ISO 13485, IATF16949, and UL, ensuring that every medical waterproof wiring harness meets the highest global standards. The manufacturing process begins with meticulous design, using 3D simulation to predict stress points and fluid exposure. We select materials such as medical-grade PVC, cross-linked polyethylene, and PTFE for their excellent chemical resistance and dielectric properties. Each harness is equipped with IP67 or higher rated connectors, preventing water ingress and ensuring continuity even during sterilization. Our quality control includes 100% electrical testing and visual inspection, achieving a 98% qualified rate. The application of our medical waterproof wiring harness extends to wearables, surgical robots, and imaging systems. For instance, our harness in a portable defibrillator reduced weight by 15% while maintaining high voltage capability. We have delivered over 500,000 harnesses for intravenous pumps, demonstrating consistent performance with zero recalls. Our global clients, including top US and European equipment makers, rely on our agile supply chain, with order lead times averaging 15 days for samples and 30 days for mass production. By adopting lean manufacturing and automated soldering, we ensure cost-effectiveness without compromising safety. As we look to the future, we are integrating IoT capabilities into our harnesses for remote monitoring, thus enhancing predictive maintenance. This dedication to innovation and quality positions us as a trusted partner in the medical industry, committed to advancing patient care through reliable interconnect solutions.

Frequently Asked Questions

What makes a wiring harness specifically "medical waterproof"?

A medical waterproof wiring harness is designed to withstand exposure to fluids, disinfectants, and sterilization processes commonly found in healthcare settings. Unlike standard harnesses, it uses medical-grade insulation materials like PTFE or cross-linked polyethylene, and features IP67 or higher ingress protection. This ensures electrical integrity and prevents corrosion, crucial for patient safety. Our harnesses are validated for compatibility with agents such as alcohol, hydrogen peroxide, and autoclave conditions.
We manufacture under ISO 13485 certification for medical devices. Additionally, our processes align with IATF16949, and we hold UL recognition. Every harness is traceable from raw material to final test. We provide documentation on request, including test reports for dielectric strength, insulation resistance, and sterilization durability. Our team is well-versed in FDA and EU MDR requirements, assisting you in achieving compliance.
Absolutely. We specialize in customization. We have two production bases and a dedicated engineering team to modify designs per your specifications. Whether you need a specific wire gauge, connector (e.g., 24P, XT30), or insulation like PVC or PTFE, we can deliver. We also offer design for manufacturing (DFM) feedback to optimize your design for reliability and cost-effectiveness.
Standard sample lead time is 7-10 days, and mass production usually takes 20-30 days. We offer expedited services for urgent requirements, potentially reducing lead times by 50%. By maintaining inventory of critical raw materials and utilizing agile manufacturing techniques, we have successfully delivered emergency orders for clinical trials and equipment repair, ensuring no downtime for our clients.
Our quality assurance includes incoming material inspection, in-process checks, and 100% electrical testing. We also perform accelerated life tests, including thermal cycling and humidity exposure, to simulate years of real-world use. Our production qualified rate stands at 98%, and we offer a comprehensive warranty. We continuously monitor process capability indices (CPK) and conduct failure mode effect analysis (FMEA) to prevent defects.

Related Articles

Dongguan Nangudi Electronics Concludes Shanghai Electronica China with Focus on New Energy and AI Robotics Solutions

23

Jun

Dongguan Nangudi Electronics Concludes Shanghai Electronica China with Focus on New Energy and AI Robotics Solutions

Custom wire harness and EV cable from trusted manufacturer. Premium wiring solutions for AI robotics and new energy applications.
View More
How to Optimize Custom Wiring Harness for Small Spaces?

22

Jul

How to Optimize Custom Wiring Harness for Small Spaces?

Mastering the Design of a Compact Custom Wiring Harness In an era where technology is becoming increasingly miniaturized—from sleek consumer wearables and compact medical devices to high-performance automotive control modules—the physical...
View More
What Industries Need a Custom Wiring Harness for Systems?

10

Aug

What Industries Need a Custom Wiring Harness for Systems?

Navigating the Shift Toward Bespoke Electrical Architecture Modern industrial landscapes are evolving at a breathtaking pace, requiring electrical distribution networks that can withstand extraordinary physical and thermal demands across every challe...
View More
Benefits of Centralized Smart Home Wiring Harness Frameworks

17

Aug

Benefits of Centralized Smart Home Wiring Harness Frameworks

The Evolution of Residential Smart Infrastructure Modern residential properties are transforming at a breathtaking pace, shifting from passive living spaces into highly integrated ecosystems powered by the Internet of Things. Homeowners increasingly ...
View More

Customer Testimonials

James Anderson
Exceptional Performance in Surgical Instruments

Our surgical equipment demands absolute reliability, and the medical waterproof wiring harnesses we sourced from this manufacturer have been outstanding. The harnesses withstand our rigorous autoclaving process without any failure, and we've seen a 30% reduction in product returns. Their team's technical expertise and willingness to customize made us feel confident. We've been a customer for 5 years and plan to continue.

Sarah Chen
Long-term Reliability for Patient Monitoring Systems

After switching to their medical waterproof wiring harnesses, our patient monitors now operate flawlessly even in high-humidity ICU environments. Data from 50,000 hours of use indicates a 99.2% reliability rate, up from 94%. Their quick prototyping allowed us to meet a critical product launch deadline. Their quality control is top-notch, and they provide excellent after-sales support.

Get a Free Quote

Our representative will contact you soon.
Email
Mobile/WhatsApp
Name
Company Name
Message
0/1000
Uncompromising Quality with 98% Qualified Rate and Global Certifications

Uncompromising Quality with 98% Qualified Rate and Global Certifications

Our medical waterproof wiring harnesses are synonymous with exceptional quality, evidenced by our 98% product qualified rate, backed by lean manufacturing processes and Six Sigma methodologies. We hold certifications such as ISO 13485, IATF16949, and UL, which are critical for medical device manufacturers. This commitment to quality ensures that our harnesses perform reliably in life-saving applications, reducing the risk of equipment failure. For instance, a recent batch of 100,000 harnesses delivered to a leading ventilator manufacturer achieved field failure rates lower than 0.1%. By partnering with us, you gain a reliable supplier that helps you maintain the highest standards and regulatory compliance, ensuring patient safety and enhancing your brand reputation globally.
Advanced Custom R&D with Over 40 Patents and a 35-Expert Team

Advanced Custom R&D with Over 40 Patents and a 35-Expert Team

Backed by nearly twenty years of specialized industrial engineering expertise, our dedicated research and development division comprising 35 senior technical professionals and an intellectual property portfolio exceeding 40 active patents establishes us as your premier innovation partner for advanced medical interconnect engineering. We deliver comprehensive custom design capabilities tailored specifically to your project requirements—ranging from the precise selection of biocompatible insulation materials such as medical-grade PTFE and cross-linked polyethylene to optimizing complex connector configurations for complete moisture and fluid ingress protection. For example, our engineering group recently collaborated directly with a pioneering surgical robotics enterprise to co-develop an ultra-compact, hermetically sealed wiring harness engineered to withstand aggressive hospital sterilization protocols.