The Evolution and Engineering of Medical Waterproof Wiring Harnesses
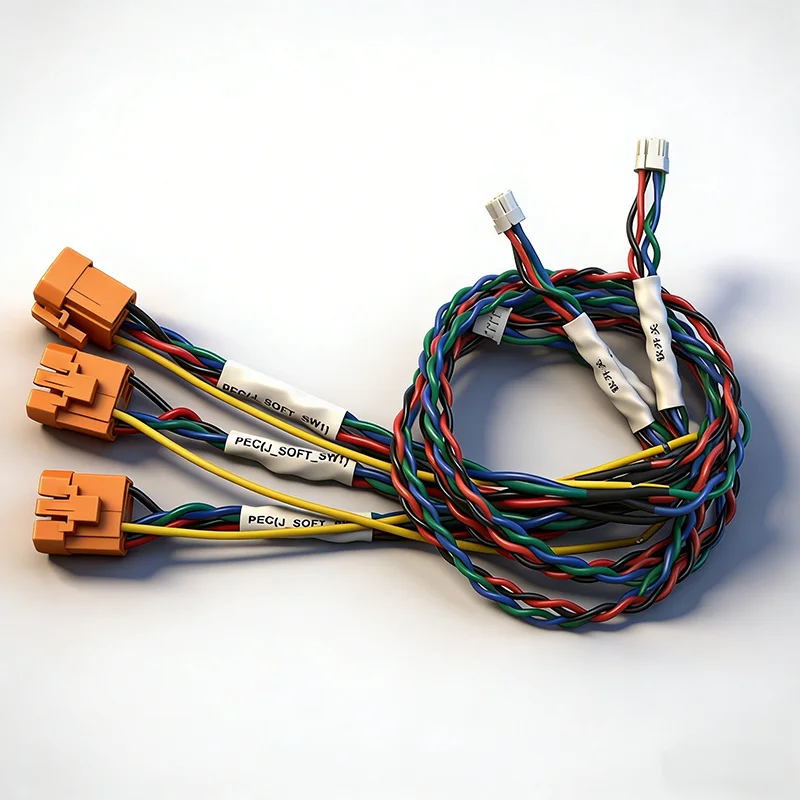
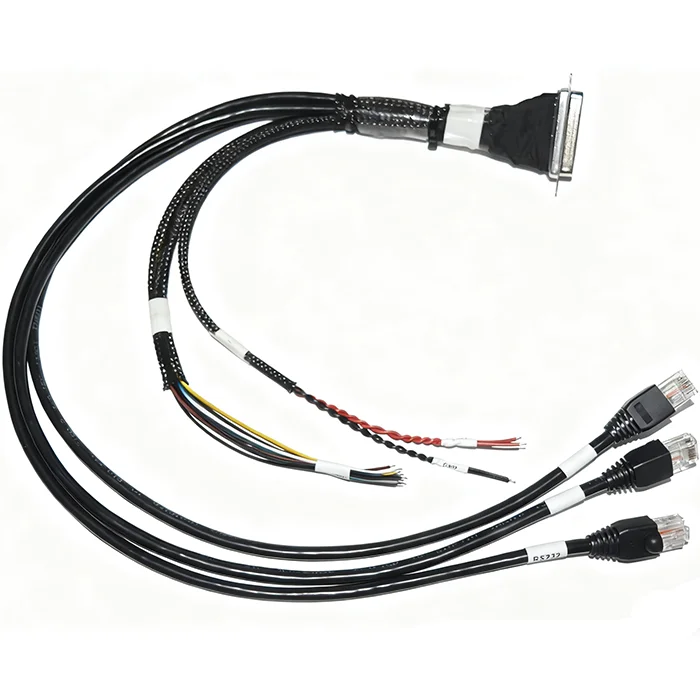
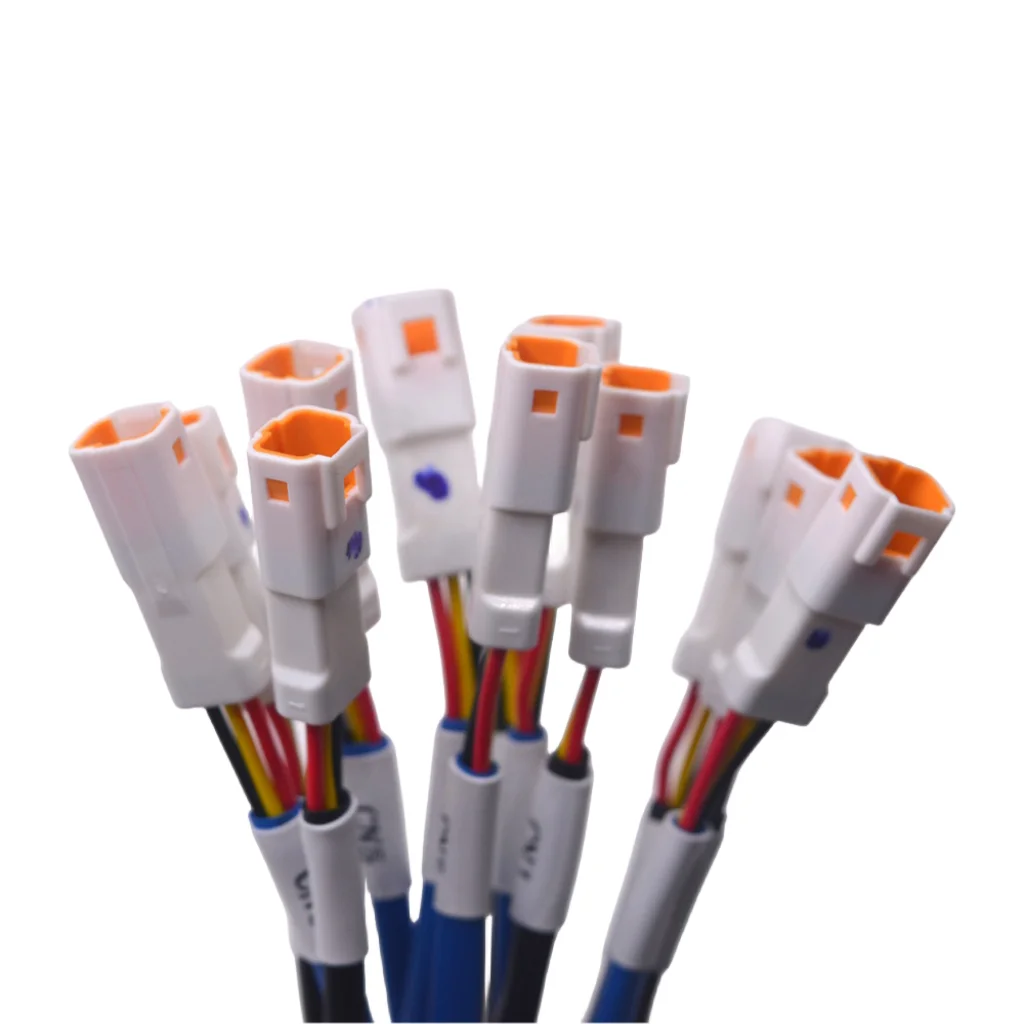
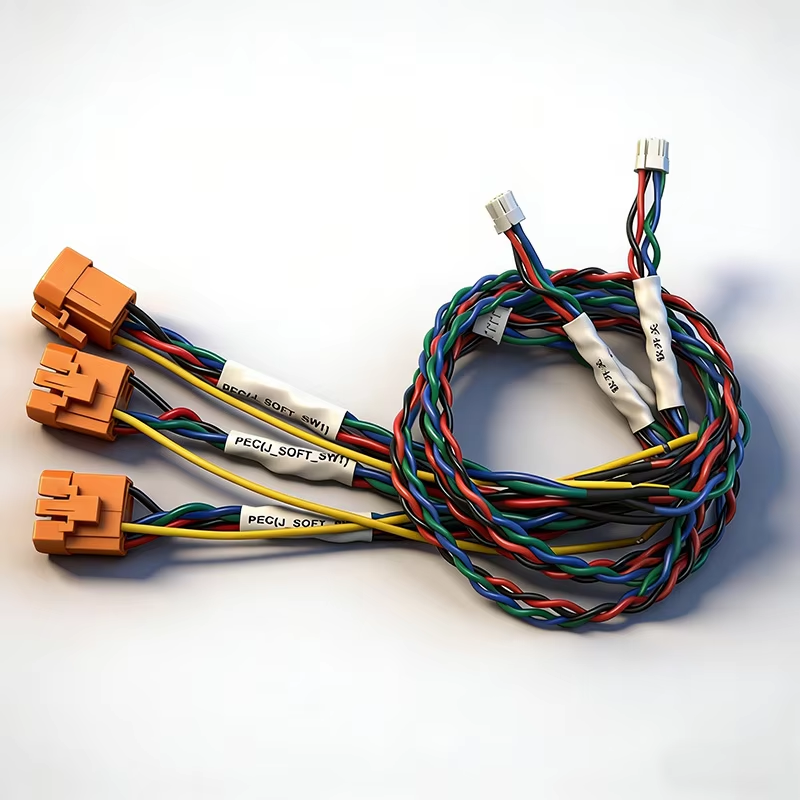
In the realm of medical technology, the medical waterproof wiring harness is an unsung hero, ensuring that devices function flawlessly in wet, sterile, and demanding environments. Over the past two decades, our company, founded in 2006, has pioneered the development of such specialized harnesses, responding to the evolving needs of healthcare providers worldwide. As a national high-tech enterprise and a "Little Giant" in Guangdong Province, we have invested heavily in R&D, holding over 40 patents and employing a team of 35 technical experts who average 10+ years of industry experience. Our production facilities, spanning 10,000 square meters, are certified under ISO 9001, ISO 13485, IATF16949, and UL, ensuring that every medical waterproof wiring harness meets the highest global standards. The manufacturing process begins with meticulous design, using 3D simulation to predict stress points and fluid exposure. We select materials such as medical-grade PVC, cross-linked polyethylene, and PTFE for their excellent chemical resistance and dielectric properties. Each harness is equipped with IP67 or higher rated connectors, preventing water ingress and ensuring continuity even during sterilization. Our quality control includes 100% electrical testing and visual inspection, achieving a 98% qualified rate. The application of our medical waterproof wiring harness extends to wearables, surgical robots, and imaging systems. For instance, our harness in a portable defibrillator reduced weight by 15% while maintaining high voltage capability. We have delivered over 500,000 harnesses for intravenous pumps, demonstrating consistent performance with zero recalls. Our global clients, including top US and European equipment makers, rely on our agile supply chain, with order lead times averaging 15 days for samples and 30 days for mass production. By adopting lean manufacturing and automated soldering, we ensure cost-effectiveness without compromising safety. As we look to the future, we are integrating IoT capabilities into our harnesses for remote monitoring, thus enhancing predictive maintenance. This dedication to innovation and quality positions us as a trusted partner in the medical industry, committed to advancing patient care through reliable interconnect solutions.