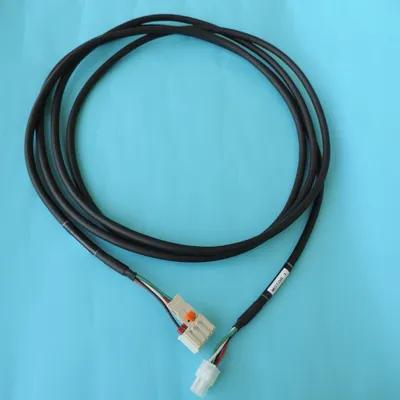
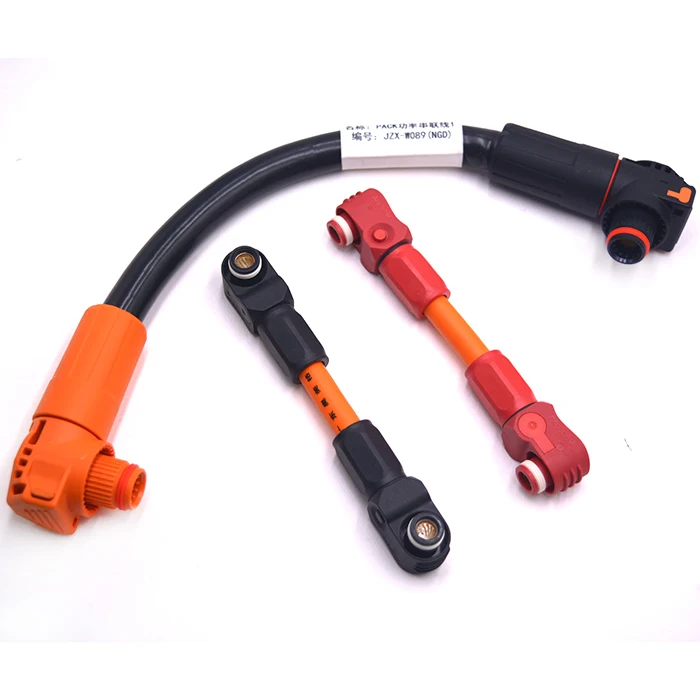
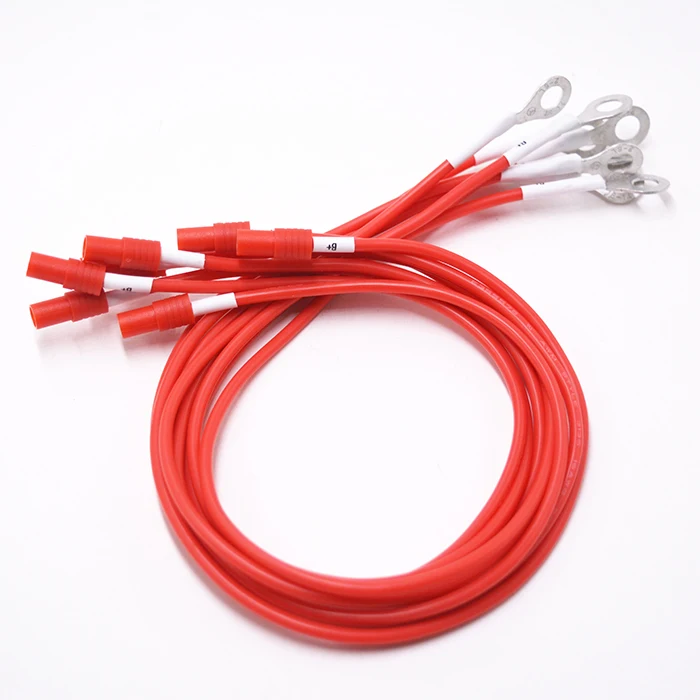
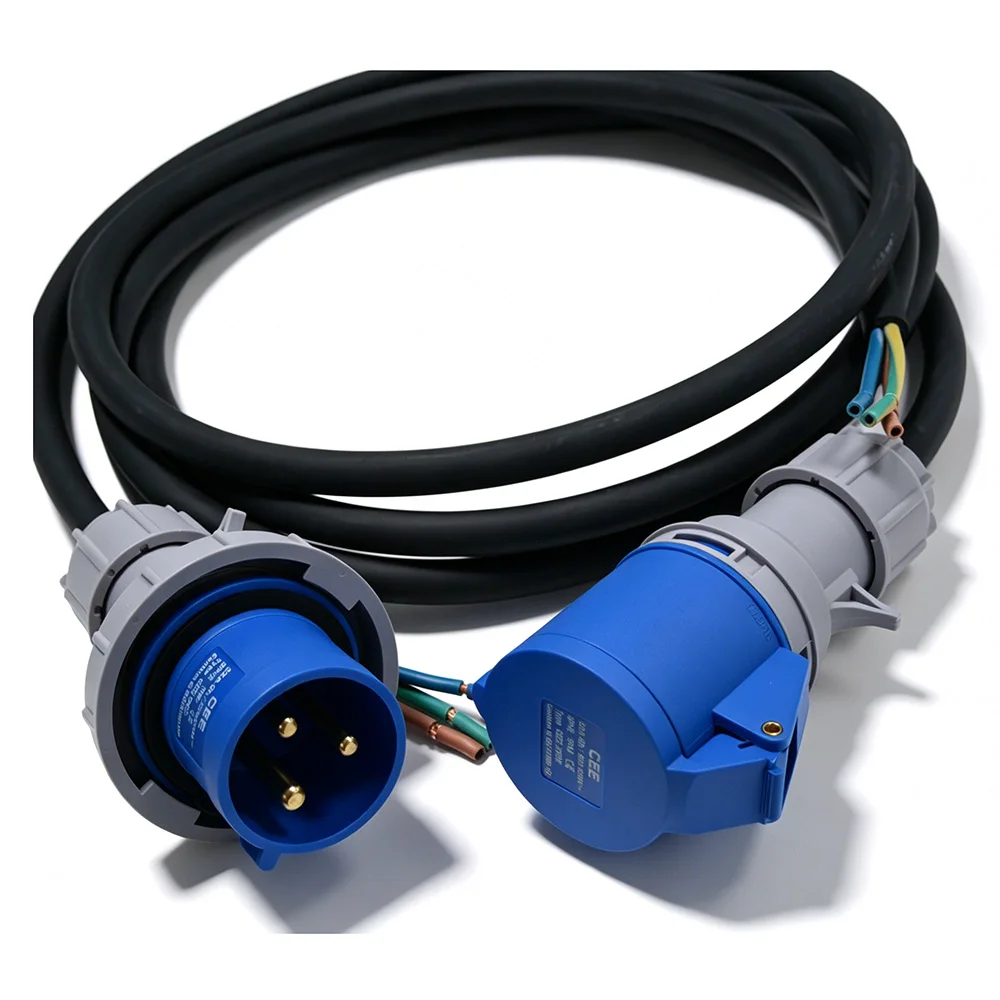
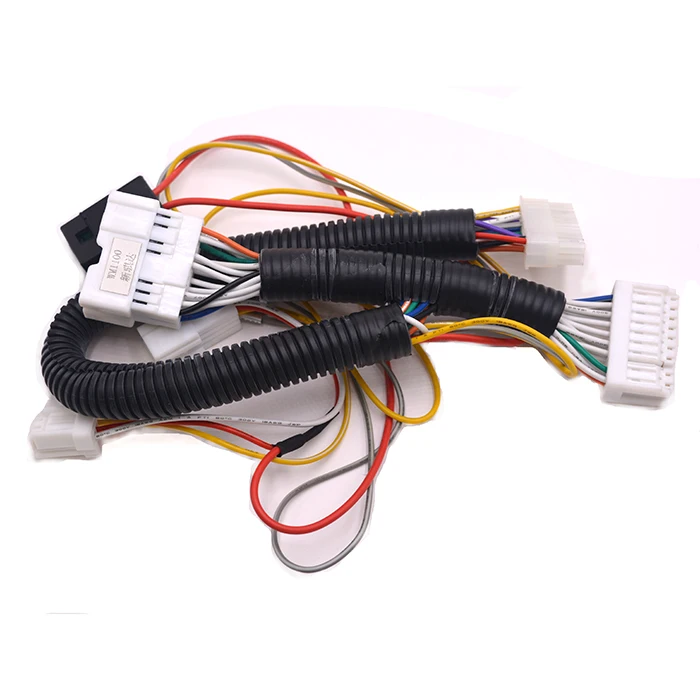
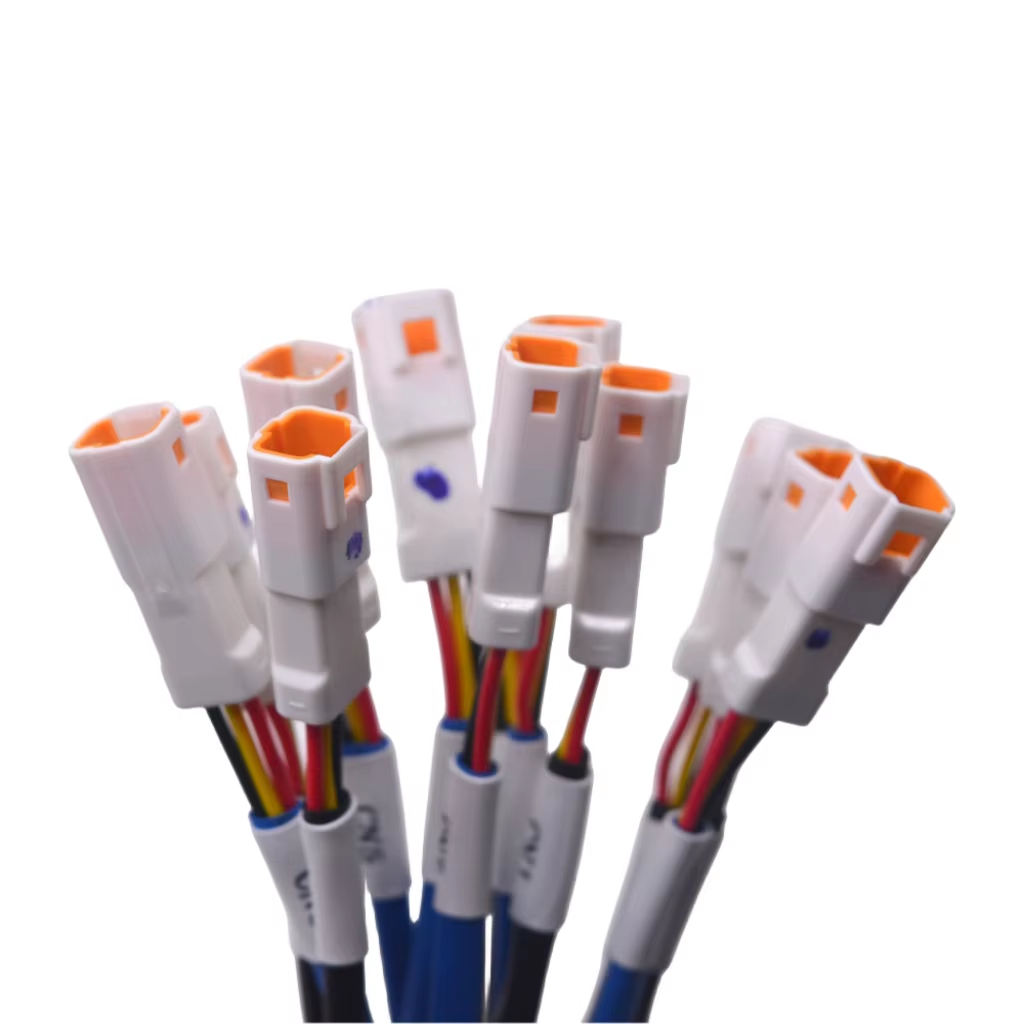
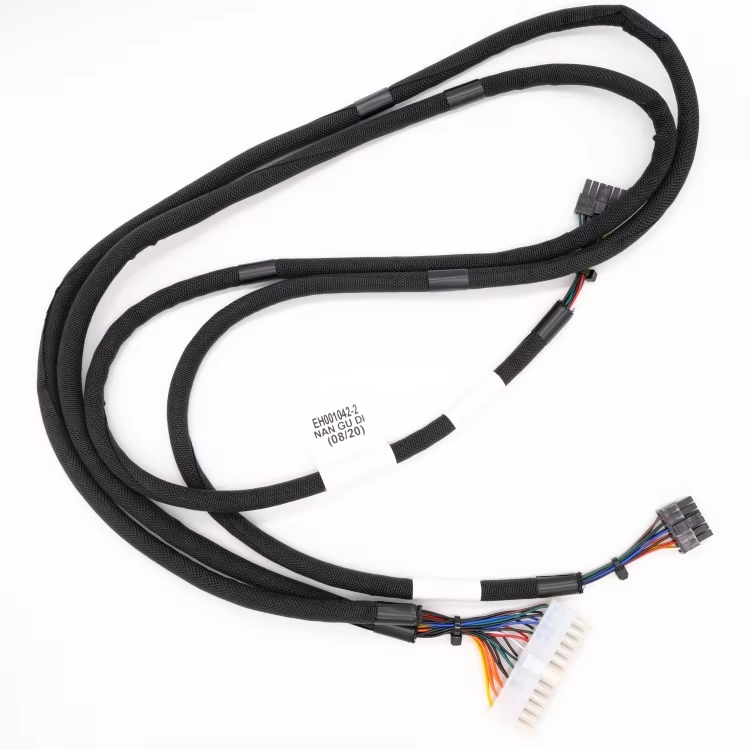
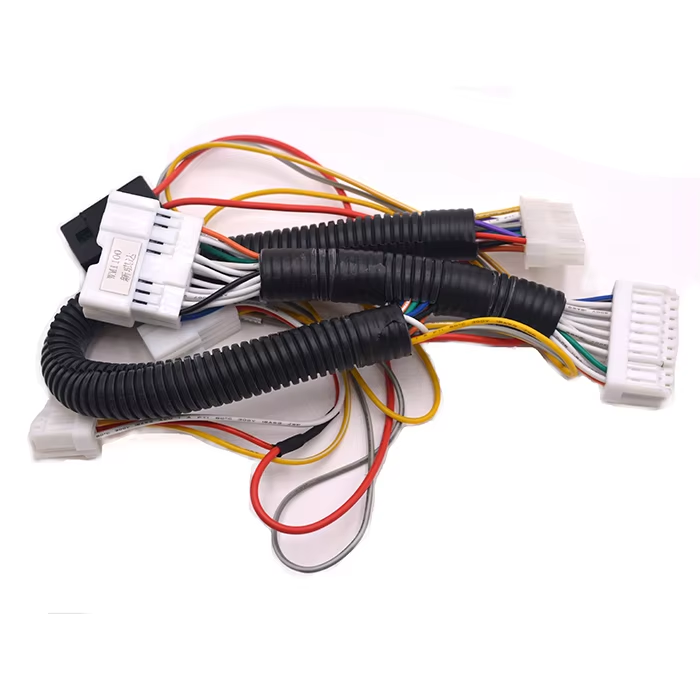
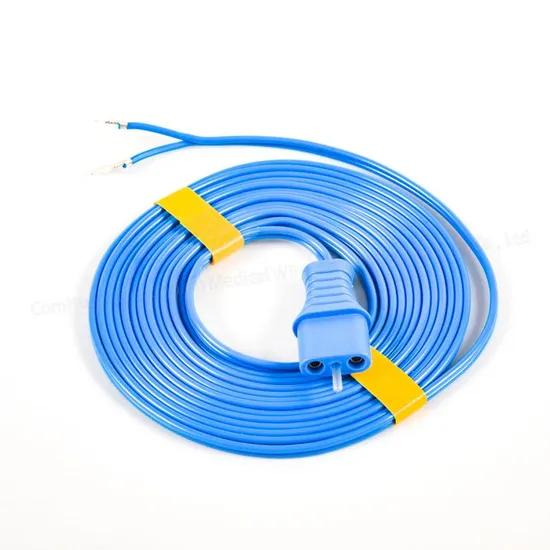
The medical wire harness is an integral component in the rapidly evolving healthcare technology sector, serving as the vital link between electrical systems and patient care devices. In an era where precision and reliability are paramount, the demand for high-quality custom wire harnesses has surged. At WEITAI, we have dedicated nearly two decades to mastering the art of wire harness manufacturing, ensuring that each product meets the stringent requirements of medical applications.
Our production process begins with rigorous material selection, using only medical-grade PVC, PTFE, and other biocompatible insulations that meet ISO 10993 standards for skin contact and biocompatibility. We employ advanced CNC wire stripping and crimping machines that ensure consistent tolerances, critical for maintaining signal integrity. Each harness undergoes a 100% electrical test using automated testing equipment that checks continuity, insulation resistance, and high-voltage withstand, guaranteeing a 98% product qualified rate as a baseline.
Our factory boasts a 12,000 square meter production area, equipped with cleanrooms that adhere to Class 100,000 standards, minimizing contamination risks for sensitive medical applications. We maintain ISO9001, ISO13485, IATF16949, and UL certifications, reflecting our commitment to quality and continuous improvement. Our team of 35 R&D professionals, each averaging over 10 years of experience, collaborates with clients to develop custom solutions tailored to specific clinical needs.
In a recent collaboration with a European medical device manufacturer, we developed a wire harness for an MRI-compatible monitoring system. By utilizing non-ferromagnetic materials and implementing a specialized shielding braid, we achieved MRI compatibility without compromising performance. The resulting harness reduced signal interference by 35% and was delivered within a strict timeline, enabling our client to meet their regulatory filing deadlines. This case exemplifies how our expertise in materials science and precision manufacturing translates into tangible client benefits.
Another notable application is in the realm of wearable health devices, where size and flexibility are critical. Our ultra-thin, multi-conductor harnesses allow for comfortable integration into clothing and patches. We have supplied harnesses used in continuous glucose monitoring systems that accurately transmit data to smartphones, improving diabetes management for patients worldwide. With an annual production capacity of over 5 million wire harnesses, we are well-positioned to support both low-volume startups and high-volume OEMs.
We pride ourselves on being a one-stop partner for custom wire harness needs, offering rapid prototyping with 48-hour sampling and scalable mass production. Our global logistics capabilities, including two production bases in Dongguan and a sales subsidiary in Hong Kong, ensure efficient delivery to clients across North America, Europe, and Asia. We understand that in the medical field, there is no room for error. That is why we have implemented a robust traceability system, allowing every harness to be traced back to its raw materials and production batch.
In conclusion, choosing the right medical wire harness partner is crucial for the success of your medical device. Our combination of technical expertise, certified production processes, and patient-centric approach makes us the ideal choice for companies aiming to innovate in healthcare. By focusing on quality, compliance, and collaboration, we help our clients bring safe and effective medical devices to market faster, ultimately improving patient outcomes globally.

 EN